New
DISCOUNTED
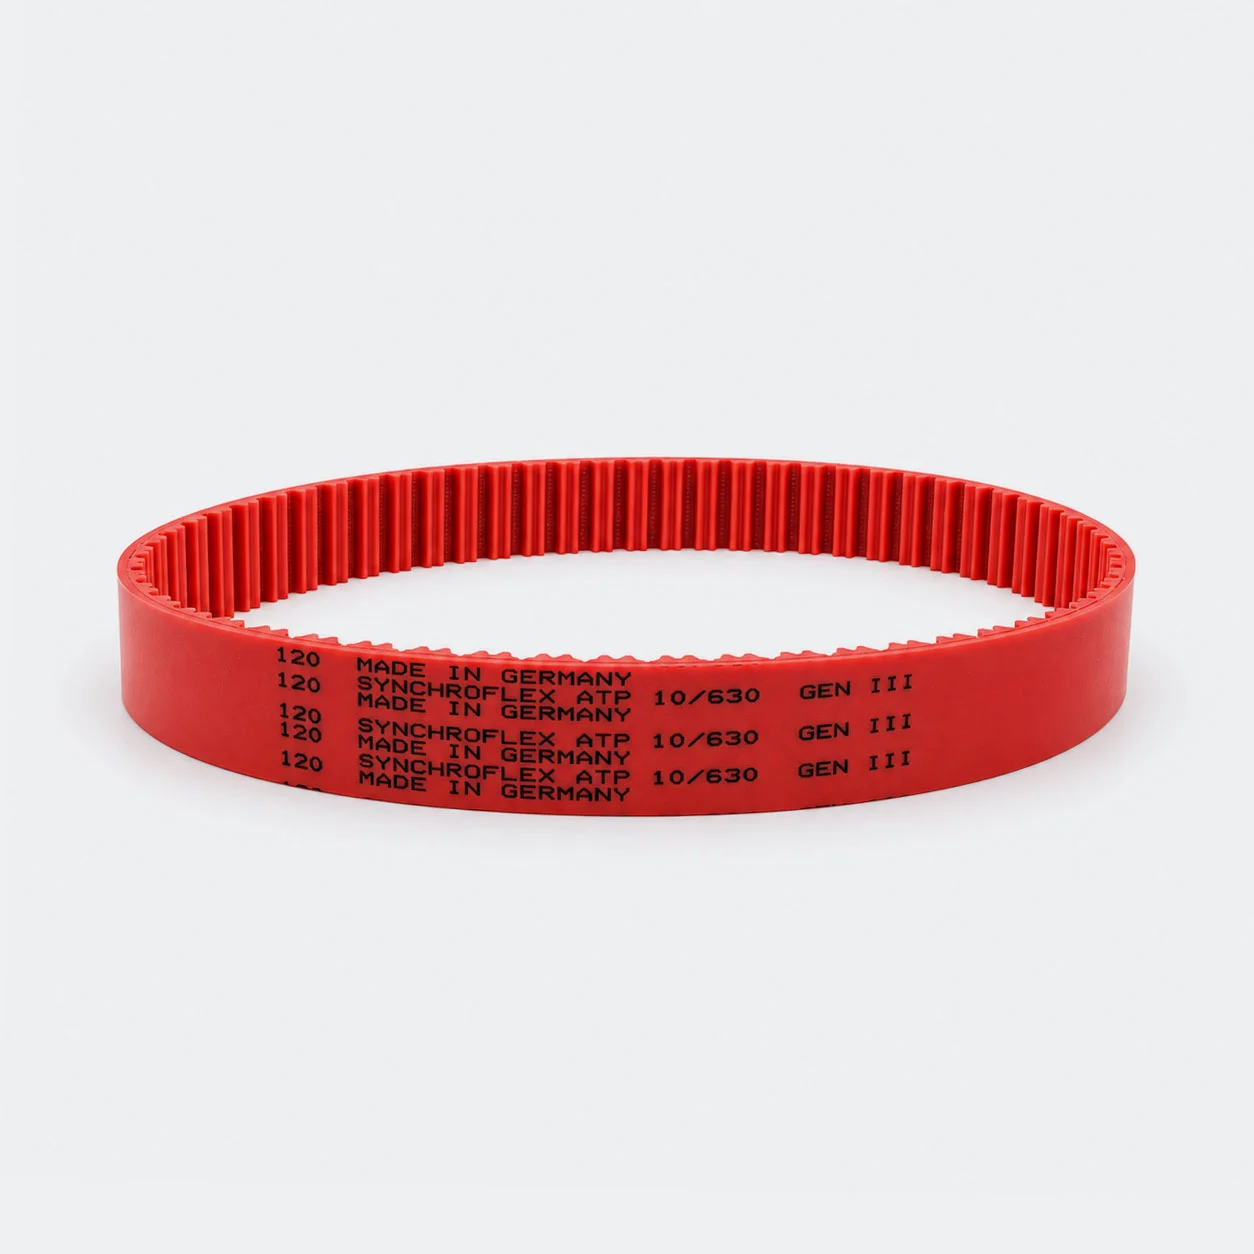
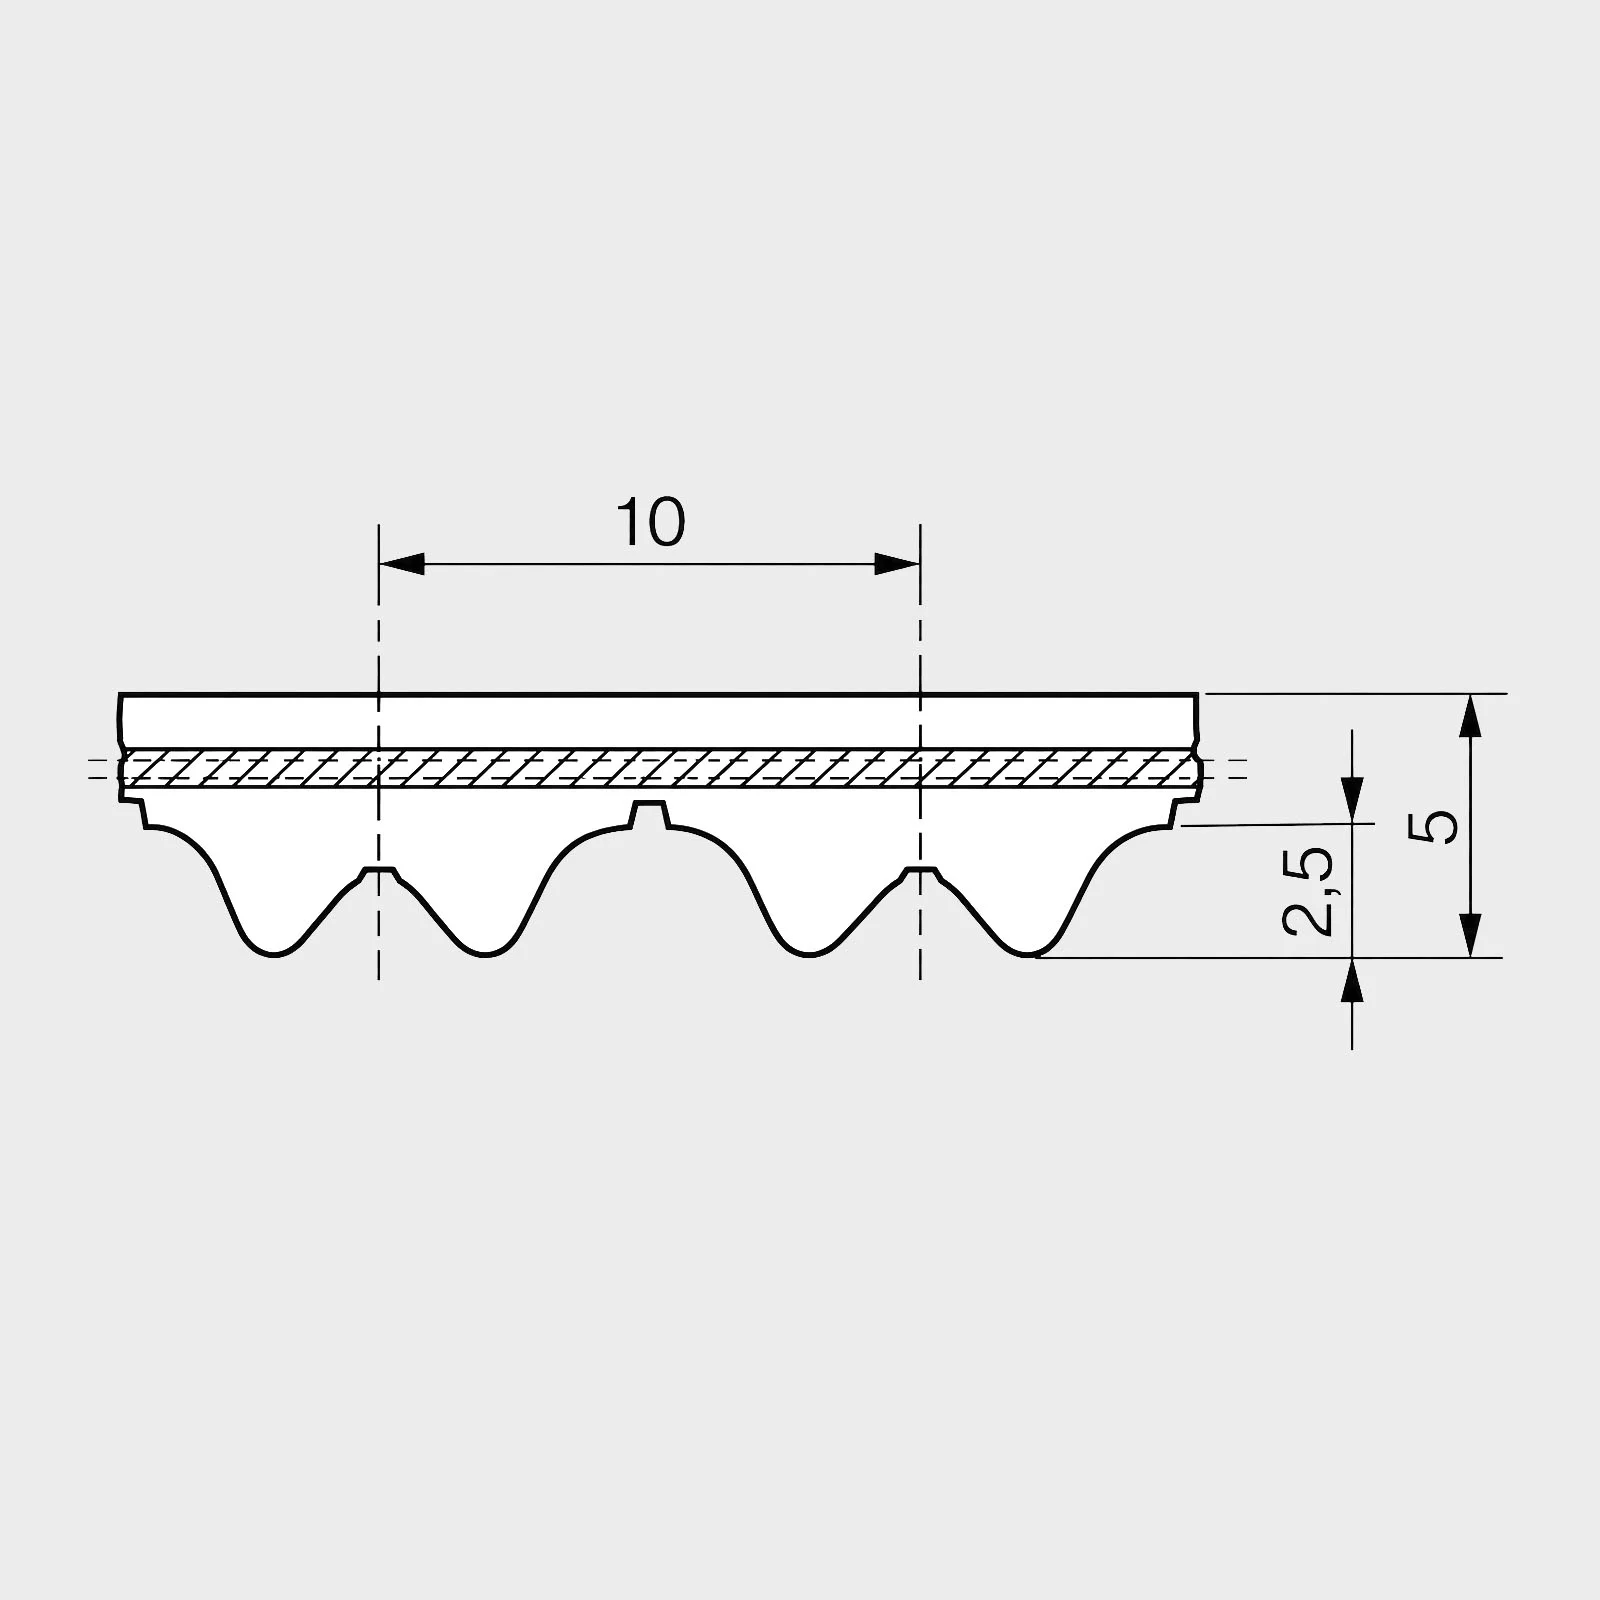



The Conti Synchroflex ATP10 GEN III 1650 combines a precise ATP10 GEN III tooth geometry with a molded polyurethane body and longitudinally stable steel cord tension elements. The product has 165 teeth and a 1650 mm pitch length, which corresponds to a tooth pitch of 10 mm. The belt is used in synchronous drives where uniform movement and reproducible position are more important than the elasticity normally associated with a conventional V-belt or flat belt. The GEN III version is the reinforced high-performance construction with red high-performance polyurethane and a denser, two-filament steel cord. It should therefore be treated as a separate product series and not as the usual standard version.
The list gathers the information normally used to identify a timing belt: nominal length, number of teeth, profile, material and make. It is important to read all the information together. Two belts can have the same pitch length but be incompatible if the tooth profile or tooth pitch is different. Conversely, a different width does not change the number of teeth as long as the profile and pitch length are the same.
The ATP profile is a further development of the high-capacity profiles, where the original trapezoidal tooth is divided into two load-bearing tooth parts. This increases the active tooth surface and provides a more uniform load distribution in the engagement. The catalogue also highlights reduced polygon effect, lower engagement noise and longer service life as key design objectives. The ATP10 will run on discs designed for the ATP10 profile.
Conti Synchroflex is manufactured by casting, where the polyurethane is precisely shaped to the tool's tooth geometry around the embedded steel cord tension elements. The casting process provides high pitch accuracy over the entire circumference of the belt and a strong connection between PU and cord. The finished timing belt is endless and therefore has no welded joints. The polyurethane provides a wear-resistant tooth and back surface, while the steel cord takes the longitudinal tensile load.
In the GEN III series, both the polyurethane and the tension body are optimized for higher performance. The tighter cord packing can increase the permissible tensile load, and the balanced two-filament construction is designed to reduce flange friction and improve belt running. Continental states that existing standard AT or ATP pulleys can be used with the corresponding GEN III profile. However, the remaining dimensioning of the drive still needs to be checked.
The basic price applies to 16 mm, and the other widths are calculated with the same percentage logic as the existing PU timing belts in the webshop. Integer widths from 16 to 50 mm can be selected on this product page. A width of twice the basic width therefore costs 100% more, while a width of one and a half times the basic width gives approximately a 50% surcharge. This price rule is a webshop calculation; it does not replace a technical dimensioning of the belt's load-bearing capacity.
The application examples in the catalogue include machine tools, grinding machines, textile machines and power transmissions with high demands on the tooth load. This shows that the profile can be used in both power transmission and motion control. However, the specific belt must only be finally selected when the machine's torque, speed, center distance and pulley geometry are known. When simply replacing a spare part, the safest method is usually to copy the documented profile, length, design and width.
It is not enough to compare the total circumference of a belt. The correct replacement must have the same pitch, tooth profile and number of teeth as the existing drive. The width must match the pulleys and the required capacity, and a DL or GEN III version must be identified separately. If in doubt, pictures of the marking, tooth profile and pulleys can be used as a supplement, but a documented spare part designation is best.
The pulleys and belt should be considered as a single tooth engagement. Correct ATP10 GEN III geometry ensures that the load is distributed across the tooth flanks rather than concentrated on tooth tips or edges. The drive ratio is selected by the number of teeth on the pulleys, while the belt's 165 teeth and 1650 mm pitch length determine the required combination of pulleys and center distance. When changing the drive, the geometry should be calculated.
The belt must be able to be placed on the pulleys without force. If it can only be mounted by forcing it over a flange, the center distance or mounting procedure is incorrect. The pulley shafts must be aligned and the flanges must be smooth and undamaged. In the case of multi-shaft or counter-bent drives, the diameter and position of the rollers must be assessed separately. Correct pretensioning reduces the risk of tooth skipping without unnecessarily loading the bearings.
Uniform light polishing of the tooth flanks may be normal, but localised spalling, ctiming baring or severe wear should be investigated. Wear on one edge often indicates misalignment or persistent flange contact. Damage to tooth tips may be due to incorrect profile, foreign bodies or inadequate engagement. If cord becomes visible or the belt has a sharp break, it should not continue in service without assessment.
Continental specifies a temperature range of up to +100 °C for the GEN III series. When operating close to the temperature limits, the drive must still be dimensioned according to the specific load and environmental conditions. The cast PU belt is maintenance-friendly and does not require lubricant. Regular visual inspection is still relevant: look for ctiming bars, frayed edges, shiny tooth flanks, foreign body impressions and abnormal side contact. Sudden changes in noise or grooveing can be signs of misalignment, too low tension or worn pulleys.
The steel cord tension members absorb the longitudinal tensile load and provide high longitudinal stiffness. This helps maintain pitch and position during operation. The cord must not be kinked, exposed or damaged during installation, as local damage can weaken the belt.
Store the belt in a dry, clean place away from direct sunlight, ozone, strong heat or chemical fumes. It should be free from sharp bends and without heavy loads on top. Avoid hanging a small belt over a sharp hook as this can cause local deformation.
Correct pretension keeps the teeth in stable engagement and reduces the risk of tooth jump. Too low a tension can cause impact and jump under load, while too high a tension increases the load on the cord, pulleys and bearings. The correct value must be determined based on the drive's dimensioning.
The documented supplier widths for this size include 16, 25 and 32 mm. The product page may also show intermediate sizes as cut widths when they are within the allowed range. This does not change the tooth profile or length, but the price is calculated based on the base width.
Misalignment can cause the belt to wander towards a flange, causing edge pressure, heat and wear damage. It can also affect tooth engagement and reduce service life. Check both the parallelism of the shafts and the alignment of the pulleys.
Noise can be caused by incorrect pretension, skewed pulleys, poor tooth profile compatibility, excessive speed, resonance or worn tooth grooves. Lubrication is not the solution. First check alignment, tension, pulley condition and whether the belt runs without abnormal side contact.
The pitch length is the nominal length measured in the belt cord line where the steel cord tension elements are located. It is not the same as a random outer circumference measurement. For this belt, 1650 mm pitch length corresponds to 165 teeth with 10 mm tooth pitch.
In summary, this is a Conti Synchroflex PU timing belt with a fixed geometry of 10 mm pitch, 165 teeth and 1650 mm pitch length. The width is selected separately, but does not change the length or number of teeth. A safe replacement requires that the entire designation and the specific version match the machine documentation.