New
DISCOUNTED
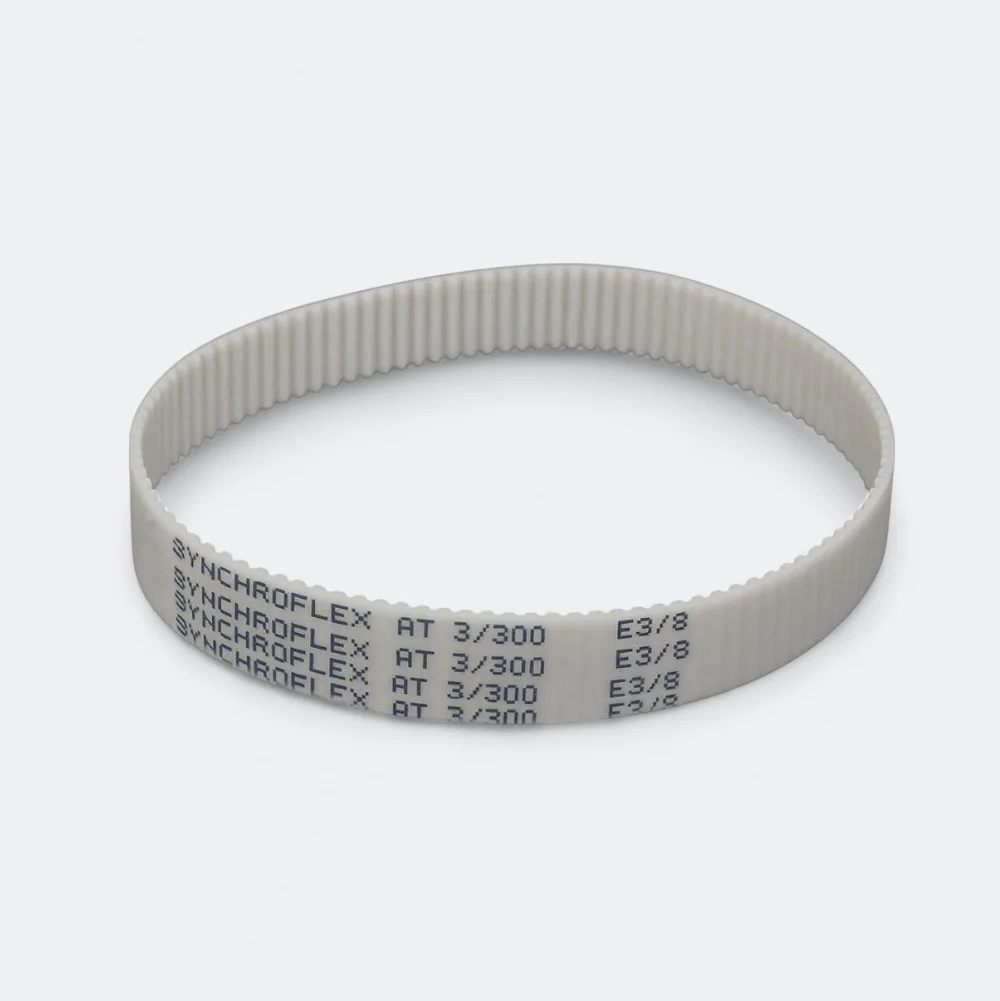


With 167 teeth spread over a pitch length of 501 mm, the Conti Synchroflex AT3 501 is designed for precise transmission of rotation, timing and position. The belt is cast endlessly in PU and has integrated steel cord tension elements that stabilize the length during normal operation. The nominal tooth pitch is 3 mm and the tooth profile must match the profile of the pulleys exactly. It is not sufficient for another belt to have approximately the same length or width. This is the standard version in the specified profile. It must not be confused with a possible GEN III version or a double-sided DL belt with the same pitch length.
These specifications can be used as a check against the marking on the old belt or against the machine's spare parts list. The pitch length is not necessarily the same as a measurement across the outside of the belt, and the number of teeth is therefore often the safest additional check. If in doubt, both the belt and timing belt pulleys should be examined before ordering a replacement.
The metric AT geometry has trapezoidal teeth with a larger tooth volume than the standard T profile. The purpose is to distribute the load advantageously in the tooth mesh and achieve higher tooth strength without making the drive unnecessarily large. The profile requires suitable AT timing belt pulleys with the same pitch; a visual similarity to other profiles is not evidence of compatibility.
The endless PU construction combines low dead weight with high longitudinal rigidity. The steel cord tension elements are cast into the belt and are not intended to be exposed, damaged or sharply broken during installation. The wear resistance of the polyurethane and the strong bond to the cord are central to the belt's lifespan. Correct handling is therefore just as important as the correct choice of profile and length.
This item is a single-sided standard design. The teeth are located on the inside of the belt, while the back is smooth. It should not be confused with a double-sided DL version or the red GEN III series. If the machine is originally dimensioned for a specific variant, a change should only be made after a technical assessment of load, pulleys and preload.
Continental cites small power drives, handling equipment, compact positioning axes and light synchronous drives as examples for this profile family. The examples describe the general application area of the profile, but are not an approval for any specific installation. The final belt width and pretension must be selected based on the transmitted torque, starting and shock loads, operating time, pulley sizes, speed and the number of teeth in simultaneous engagement. For safety-critical or heavily loaded drives, an actual calculation should be made.
The pulleys and belt should be considered as a single tooth engagement. Correct AT3 geometry ensures that the load is distributed across the tooth flanks rather than concentrated on tooth tips or edges. The drive ratio is selected by the number of teeth on the pulleys, while the belt's 167 teeth and 501 mm pitch length determine the required combination of pulleys and center distance. When changing the drive, the geometry should be calculated.
When installing, the cord pullers must be protected against kinks and local pressure damage. The belt must not be pinched with pliers or a screwdriver, and it should not be folded sharply. Check that the pulleys have the same pitch and profile as the belt and that they are not worn out. A stable drive is achieved through the right combination of alignment, wrapping and calculated pretension.
This product line has been created with 6 mm as the base width because this is the width of the selected item and thus the SKU used for inventory control. Integer widths from 6 to 50 mm can be selected on this product page. The widths that appear as standard widths in the supplier data are marked separately in the options. The price surcharge is calculated as a percentage of the base width: doubling the width results in a surcharge of 100%. The technically necessary width should be selected according to the load and not only according to the price.
Uniform light polishing of the tooth flanks may be normal, but localised spalling, ctiming baring or severe wear should be investigated. Wear on one edge often indicates misalignment or persistent flange contact. Damage to tooth tips may be due to incorrect profile, foreign bodies or inadequate engagement. If cord becomes visible or the belt has a sharp break, it should not continue in service without assessment.
The standard material is specified for ambient temperatures from -30 °C to +80 °C. Applications close to the limits, especially below -10 °C or above +50 °C, may require special sizing. The service life is not only affected by the material, but also by load peaks, bending, pulley size, alignment and environment. Keep the drive clean and do not remove deposits with sharp tools that could damage the teeth. If the belt operates in chemically exposed areas, food environments, clean rooms or at extreme temperatures, a suitable special design should be considered.
It is not enough to compare the total circumference of a belt. The correct replacement must have the same pitch, tooth profile and number of teeth as the existing drive. The width must match the pulleys and the required capacity, and a DL or GEN III version must be identified separately. If in doubt, pictures of the marking, tooth profile and pulleys can be used as a supplement, but a documented spare part designation is best.
No. A timing belt requires timing belt pulleys with the correct profile and pitch, while a V-belt works by friction in V-grooves. A conversion therefore requires new pulleys and a dimensioning of the entire transmission. The product is intended as a timing belt, not as a universal replacement.
Count the teeth and check the pitch. 167 teeth times 3 mm gives 501 mm pitch length. Then compare the profile and design with the marking or the machine parts list. A measurement around the outside of the belt alone is not accurate enough.
The possibility depends on the profile, cord design, the diameter of the rollers and the specific belt routing. Counter-bending increases the bending load and must be included in the dimensioning. A roller on the belt back must have sufficient diameter and be positioned so that tooth engagement and grooveing are not impaired.
Check that the belt runs centrally, that there is no abnormal heat or noise, and that the edges are not constantly rubbing against the flanges. Also look for signs of too low or too high pretension. If the drive requires a re-tension check, the machine manufacturer's procedure must be followed.
Not necessarily. A larger width provides a more active belt cross-section and can increase the permissible load, but the drive capacity also depends on the profile, number of teeth in mesh, pulley size, speed, load factor and preload. The width should be selected by an overall calculation.
Store the belt in a dry, clean place away from direct sunlight, ozone, strong heat or chemical fumes. It should be free from sharp bends and without heavy loads on top. Avoid hanging a small belt over a sharp hook as this can cause local deformation.
Noise can be caused by incorrect pretension, skewed pulleys, poor tooth profile compatibility, excessive speed, resonance or worn tooth grooves. Lubrication is not the solution. First check alignment, tension, pulley condition and whether the belt runs without abnormal side contact.
In summary, this is a Conti Synchroflex PU timing belt with a fixed geometry of 3 mm pitch, 167 teeth and 501 mm pitch length. The width is selected separately, but does not change the length or number of teeth. A safe replacement requires that the entire designation and the specific version match the machine documentation.