New
DISCOUNTED
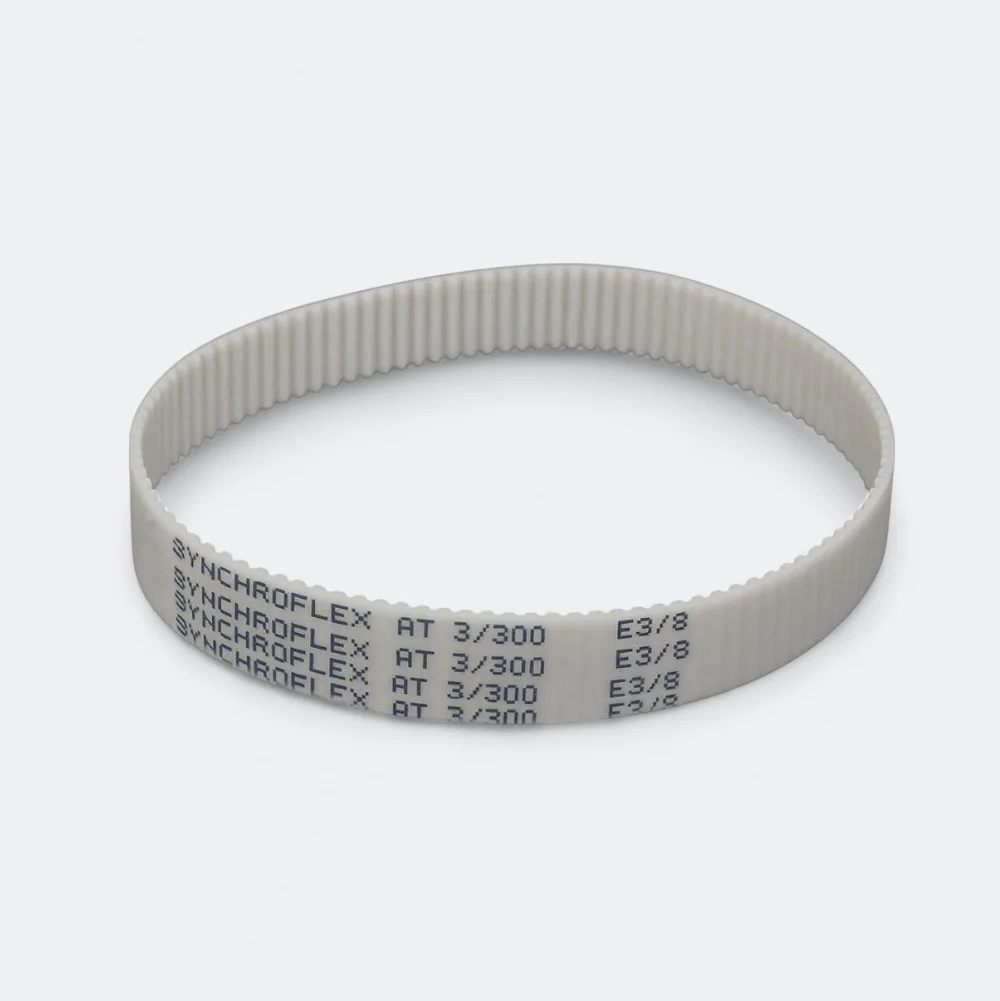


This AT3 timing belt is specified with a pitch length of 450 mm and 150 teeth. The ratio between length and number of teeth is fixed: 450 mm divided by 3 mm gives exactly 150 teeth. The Conti Synchroflex AT3 450 is supplied as a cast, endless PU belt, so there is no weld joint in the finished ring. The design is developed for synchronous operation and precise machine movements. This is the standard version in the specified profile. It should not be confused with a possible GEN III version or a double-sided DL belt with the same pitch length.
The list gathers the information normally used to identify a timing belt: nominal length, number of teeth, profile, material and make. It is important to read all the information together. Two belts can have the same pitch length but be incompatible if the tooth profile or tooth pitch is different. Conversely, a different width does not change the number of teeth as long as the profile and pitch length are the same.
The metric AT geometry has trapezoidal teeth with a larger tooth volume than the standard T profile. The purpose is to distribute the load advantageously in the tooth mesh and achieve higher tooth strength without making the drive unnecessarily large. The profile requires suitable AT timing belt pulleys with the same pitch; a visual similarity to other profiles is not evidence of compatibility.
The endless PU construction combines low dead weight with high longitudinal rigidity. The steel cord tension elements are cast into the belt and are not intended to be exposed, damaged or sharply broken during installation. The wear resistance of the polyurethane and the strong bond to the cord are central to the belt's lifespan. Correct handling is therefore just as important as the correct choice of profile and length.
The product is the regular Conti Synchroflex standard version in the specified profile. Standard and GEN III may have the same pitch length and number of teeth, but they are different product series with different material construction and capacity data. The same applies to a DL belt, which has teeth on both sides. When reordering, the entire profile designation should therefore be checked, not just the length.
This product line has been created with 6 mm as the base width because this is the width of the selected item and thus the SKU used for inventory control. Integer widths from 6 to 50 mm can be selected on this product page. The widths that appear as standard widths in the supplier data are marked separately in the options. The price surcharge is calculated as a percentage of the base width: doubling the width results in a surcharge of 100%. The technically necessary width should be selected according to the load and not only according to the price.
Continental cites small power drives, handling equipment, compact positioning axes and light synchronous drives as examples for this profile family. The examples describe the general application area of the profile, but are not an approval for any specific installation. The final belt width and pretension must be selected based on the transmitted torque, starting and shock loads, operating time, pulley sizes, speed and the number of teeth in simultaneous engagement. For safety-critical or heavily loaded drives, an actual calculation should be made.
The product's 150 teeth provide a convenient length check. Multiplying the number of teeth by 3 mm gives a pitch length of 450 mm. If an existing belt has a different number of teeth, it is not the same size, even though it may look almost the same length. Also check that the teeth on the pulleys match the AT3; the same pitch number alone is not always sufficient.
The pulleys and belt should be considered as a single tooth engagement. Correct AT3 geometry ensures that the load is distributed over the tooth flanks rather than concentrated on tooth tips or edges. The drive ratio is selected by the number of teeth on the pulleys, while the belt's 150 teeth and 450 mm pitch length determine the required combination of pulleys and center distance. When changing the drive, the geometry should be calculated.
When installing, the cord pullers must be protected against kinks and local pressure damage. The belt must not be pinched with pliers or a screwdriver, and it should not be folded sharply. Check that the pulleys have the same pitch and profile as the belt and that they are not worn out. A stable drive is achieved through the right combination of alignment, wrapping and calculated pretension.
A properly running timing belt should move smoothly without continuous contact against one flange. Regularly check the teeth for deformation, the back for ctiming bars and the edges for frayed areas. Abnormal noise or heat can be an early sign of incorrect tension or pulley failure. A systematic check of pulleys and belt is more effective than trying to hide symptoms with lubricant.
The standard material is specified for ambient temperatures from -30 °C to +80 °C. Applications close to the limits, especially below -10 °C or above +50 °C, may require special dimensioning. The timing belt operates without lubrication, and oil or grease should therefore not be added to dampen noise. The polyurethane is described as resistant to aging as well as simple oils, grease and petrol and to certain acids and bases. In the case of permanent contact, cleaning chemicals or unknown media, material compatibility should be specifically clarified.
Pulleys should be evaluated if the tooth grooves are worn, sharp, crooked or damaged. A new belt on worn pulleys may have poor load distribution and short life. Also check flanges for bars and side contact and the grooves for foreign objects.
The standard PU is described as resistant to simple oils, grease and petrol as well as certain acids and bases. This does not mean universal chemical resistance. In the case of continuous contact, high concentrations or cleaning agents, the specific liquid, temperature and exposure time should be assessed.
Check that the belt runs centrally, that there is no abnormal heat or noise, and that the edges are not constantly rubbing against the flanges. Also look for signs of too low or too high pretension. If the drive requires a re-tension check, the machine manufacturer's procedure must be followed.
The belt has 150 teeth. The number of teeth is calculated by dividing the pitch length of 450 mm by the tooth pitch of 3 mm. The result is 150, and this number can be used as an additional check when identifying an existing belt. A different number of teeth means a different pitch length.
Not necessarily. A larger width provides a more active belt cross-section and can increase the permissible load, but the drive capacity also depends on the profile, number of teeth in mesh, pulley size, speed, load factor and preload. The width should be selected by an overall calculation.
No. A timing belt requires timing belt pulleys with the correct profile and pitch, while a V-belt works by friction in V-grooves. A conversion therefore requires new pulleys and a dimensioning of the entire transmission. The product is intended as a timing belt, not as a universal replacement.
The pitch length is the nominal length measured in the belt cord line where the steel cord tension members are located. It is not the same as a random outside circumference measurement. For this belt, 450 mm pitch length corresponds to 150 teeth with 3 mm tooth pitch.
The product brings together the specified AT3 profile and length on one side, so that the appropriate width can be selected without creating a separate item for each cut. The main technical data is 450 mm pitch length and 150 teeth. If in doubt about load or pulley compatibility, the drive should be calculated before ordering the belt.