New
DISCOUNTED


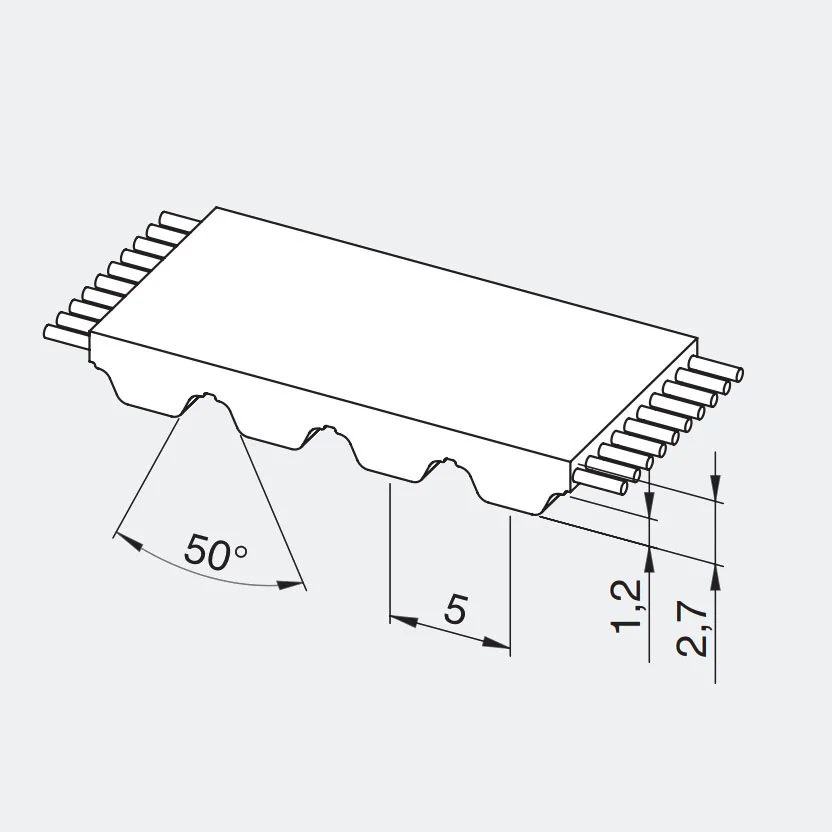




This AT5 GEN III timing belt is specified with a pitch length of 920 mm and 184 teeth. The ratio between length and number of teeth is fixed: 920 mm divided by 5 mm gives exactly 184 teeth. The Conti Synchroflex AT5 GEN III 920 is supplied as a cast, endless PU belt, so that there is no weld joint in the finished ring. The design is developed for synchronous operation and precise machine movements. The GEN III version is the reinforced high-performance design with red high-performance polyurethane and a denser, two-filament steel cord. It should therefore be treated as a separate product series and not as the regular standard version.
The technical data below describes the part of the product that does not change when a different belt width is selected. Pitch length, tooth pitch and number of teeth remain identical for all width choices. However, the width affects the available belt cross-section width and the price calculated on the product page. Correct sizing must always take into account torque, speed, number of teeth in mesh, pulley diameters, service factor and any counter-bending.
The metric AT geometry has trapezoidal teeth with a larger tooth volume than the standard T profile. The purpose is to distribute the load advantageously in the tooth mesh and achieve higher tooth strength without making the drive unnecessarily large. The profile requires suitable AT timing belt pulleys with the same pitch; a visual similarity to other profiles is not evidence of compatibility.
With the cast manufacturing method, the finished belt becomes an exact copy of a precision-machined shape. This is a major reason for the uniform tooth pitch and reproducible length. The steel cord is integrated into the polyurethane and contributes to position and angular precision. The design is suitable for synchronous drives, where a conventional elastic friction belt does not provide the desired repeatability.
In the GEN III series, both the polyurethane and the tension body are optimized for higher performance. The tighter cord packing can increase the permissible tensile load, and the balanced two-filament construction is designed to reduce flange friction and improve belt running. Continental states that existing standard AT or ATP pulleys can be used with the corresponding GEN III profile. However, the remaining dimensioning of the drive still needs to be checked.
Continental cites machine tools, pu , textile machines and positioning and conveying systems as examples for this profile family. The examples describe the general area of application of the profile, but do not constitute an approval for any specific installation. The final belt width and pretension must be selected based on the transmitted torque, starting and shock loads, operating time, pulley sizes, speed and the number of teeth in simultaneous engagement. For safety-critical or heavily loaded drives, an actual calculation should be made.
The basic price applies to 6 mm, and the other widths are calculated with the same percentage logic as the existing PU timing belts in the webshop. Integer widths from 6 to 50 mm can be selected on this product page. A width of twice the basic width therefore costs 100% more, while a width of one and a half times the basic width gives approximately 50% extra. This price rule is a webshop calculation; it does not replace a technical dimensioning of the belt's load-bearing capacity.
The tooth profile of the timing belt pulleys must correspond to the AT5 GEN III of the belt, and their pitch must be 5 mm. The transmission ratio is determined by the ratio of the number of teeth of the pulleys, not by the width of the belt. A larger pulley usually reduces the bending load, while a very small pulley gives more bending per revolution. The angle of engagement and the number of teeth in mesh must be sufficient for the current load.
The belt must be able to be placed on the pulleys without force. If it can only be mounted by forcing it over a flange, the center distance or mounting procedure is incorrect. The pulley shafts must be aligned and the flanges must be smooth and undamaged. In the case of multi-shaft or counter-bent drives, the diameter and position of the rollers must be assessed separately. Correct pretensioning reduces the risk of tooth skipping without unnecessarily loading the bearings.
It is not enough to compare the total circumference of a belt. The correct replacement must have the same pitch, tooth profile and number of teeth as the existing drive. The width must match the pulleys and the required capacity, and a DL or GEN III version must be identified separately. If in doubt, pictures of the marking, tooth profile and pulleys can be used as a supplement, but a documented spare part designation is best.
Early damage is often caused by conditions surrounding the belt rather than the material itself. Bent shafts, worn tooth grooves, foreign objects and incorrect pretensioning can all shorten the service life. In the event of a belt break, the pulleys should therefore be cleaned and inspected before the new belt is fitted. Also check whether load conditions or start-stop cycles have changed since the original design.
Continental specifies a temperature range of up to +100 °C for the GEN III series. When operating close to the temperature limits, the drive must still be dimensioned according to the specific load and environmental conditions. The cast PU belt is maintenance-friendly and does not require lubricant. Regular visual inspection is still relevant: look for ctiming bars, frayed edges, shiny tooth flanks, foreign body impressions and abnormal side contact. Sudden changes in noise or grooveing can be signs of misalignment, too low tension or worn pulleys.
6 mm is the width of the supplier item whose SKU is used as the main product's stock reference. Other widths are handled as choices under the same product because they are cut from the same type of timing belt sleeve. The base width also determines the percentage-based pricing in the webshop.
The steel cord tension members absorb the longitudinal tensile load and provide high longitudinal stiffness. This helps maintain pitch and position during operation. The cord must not be kinked, exposed or damaged during installation, as local damage can weaken the belt.
The tooth engagement provides a positive, synchronous transmission without the normal slippage of a friction belt. This makes the profile relevant for positioning tasks, but the achievable accuracy also depends on the quality of the pulleys, shaft play, belt pretension, load and the overall machine design.
This should be avoided. The belt should be installed by adjusting the center distance or following the correct installation procedure for the machine. Forcing it over a flange can damage the cord pullers, teeth or belt edge. After installation, the pulleys must be parallel and the pretension must be correct.
The tooth pitch is the distance from one tooth to the next and is 5 mm for this profile. The pitch length is the entire nominal circumference in the cord line and is 920 mm. When the pitch length is divided by the tooth pitch, the belt has 184 teeth.
No. This is a cast endless timing belt with a fixed pitch length. It can be cut to width within the available options, but the circumference and number of teeth cannot be changed. If the length needs to be changed, a different cast belt size is required.
Count the teeth and check the pitch. 184 teeth times 5 mm gives 920 mm pitch length. Then compare the profile and design with the marking or the machine's spare parts list. A measurement around the outside of the belt alone is not accurate enough.
Conti Synchroflex AT5 GEN III 920 is the correct size when the drive requires AT5 GEN III, 920 mm pitch length and 184 teeth. The belt is cast endless in PU with steel cord and must be used with timing belt pulleys that match the profile. Choose the width according to the technical load and always check the design, alignment and pretension before commissioning.