New
DISCOUNTED


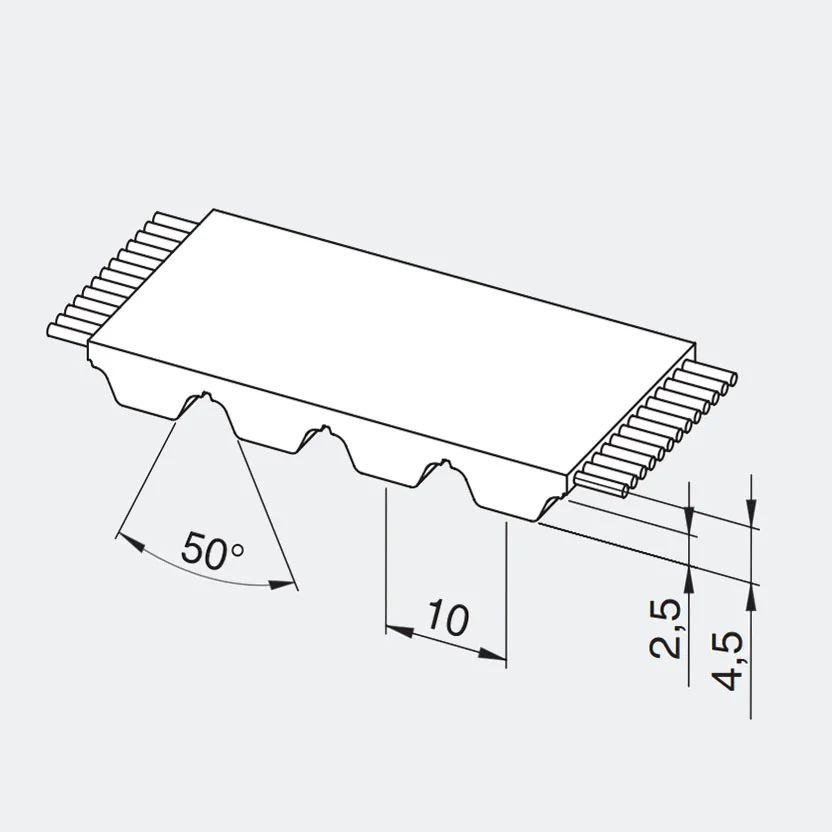




The Conti Synchroflex AT10 GEN III 1050 is an endless, cast polyurethane timing belt with 105 teeth, 10 mm tooth pitch and a pitch length of 1050 mm. It is intended for synchronous power transmission, where the driving and driven shafts must follow a fixed tooth ratio without the slippage known from friction-based belt drives. The pitch length is the nominal length measurement in the belt cord line and is therefore the measurement that must be compared with the existing belt, the machine's spare parts data and the installed timing belt pulleys. The GEN III version is the reinforced high-performance construction with red high-performance polyurethane and denser, two-filament steel cord. It should therefore be treated as a separate product series and not as the regular standard version.
The list gathers the information normally used to identify a timing belt: nominal length, number of teeth, profile, material and make. It is important to read all the information together. Two belts can have the same pitch length but be incompatible if the tooth profile or tooth pitch is different. Conversely, a different width does not change the number of teeth as long as the profile and pitch length are the same.
The metric AT geometry has trapezoidal teeth with a larger tooth volume than the standard T profile. The purpose is to distribute the load advantageously in the tooth mesh and achieve higher tooth strength without making the drive unnecessarily large. The profile requires suitable AT timing belt pulleys with the same pitch; a visual similarity to other profiles is not evidence of compatibility.
Conti Synchroflex is manufactured by casting, where the polyurethane is precisely shaped to the tool's tooth geometry around the embedded steel cord tension elements. The casting process provides high pitch accuracy over the entire circumference of the belt and a strong connection between PU and cord. The finished timing belt is endless and therefore has no welded joints. The polyurethane provides a wear-resistant tooth and back surface, while the steel cord takes the longitudinal tensile load.
The red GEN III construction is not just a color variant. It is developed with higher cord density and a special steel cord construction that provides increased tensile strength, better grooveing and the ability to carry higher loads. The catalog also specifies a temperature range up to +100 °C. Standard and GEN III must therefore be created and selected as separate products, even when the length and profile are the same.
The product's 105 teeth provide a convenient length check. Multiplying the number of teeth by 10 mm gives a pitch length of 1050 mm. If an existing belt has a different number of teeth, it is not the same size, even though it may look almost the same length. Also check that the teeth on the pulleys match the AT10 GEN III; the same pitch number alone is not always sufficient.
The application examples in the catalogue include construction machinery, pu , paper machines, compressors, compactors, textile machines and roller conveyor drives. This shows that the profile can be used in both power transmission and motion control. However, the specific belt must only be finally selected when the machine's torque, speed, center distance and pulley geometry are known. When simply replacing spare parts, the safest method is usually to copy the documented profile, length, design and width.
The belt width is not written in the product name because the same pitch length is collected on one product page. The starting pu is 16 mm. Integer widths from 16 to 50 mm can be selected on this product page. The original supplier widths for this length are 16, 20, 25, 32 and 50 mm. Other intermediate sizes are offered as cut-to-sizes of the same type of timing belt sleeve when they are within the selection shown. The number of teeth, pitch length and profile do not change when the width is changed.
A belt of the correct length can still function poorly if the pulleys have the wrong profile, are worn or are misaligned. Therefore, check the tooth grooves, flanges, shaft alignment and the number of teeth on the pulleys. For AT10 GEN III, the nominal tooth pitch is 10 mm. The fixed tooth mesh makes the gear ratio reproducible, but only when the belt has sufficient wrap and does not run with constant side pressure.
The belt must be able to be placed on the pulleys without force. If it can only be mounted by forcing it over a flange, the center distance or mounting procedure is incorrect. The pulley shafts must be aligned and the flanges must be smooth and undamaged. In the case of multi-shaft or counter-bent drives, the diameter and position of the rollers must be assessed separately. Correct pretensioning reduces the risk of tooth skipping without unnecessarily loading the bearings.
Continental specifies a temperature range of up to +100 °C for the GEN III series. When operating close to the temperature limits, the drive must still be dimensioned according to the specific load and environmental conditions. The timing belt operates without lubrication, and oil or grease should therefore not be added to dampen noise. The polyurethane is described as resistant to aging as well as simple oils, grease and petrol and to certain acids and bases. In the case of permanent contact, cleaning chemicals or unknown media, material compatibility should be specifically clarified.
Troubleshooting should start with pu location of the damage. Edge wear is typically associated with grooveing and alignment, while tooth skipping can be associated with too low tension, load peaks or too few teeth in mesh. Ctiming bars on the back can be caused by too small rollers, back bending or environmental influences. Do not simply replace the belt without also finding the mechanical cause.
Pulleys should be evaluated if the tooth grooves are worn, sharp, crooked or damaged. A new belt on worn pulleys may have poor load distribution and short life. Also check flanges for bars and side contact and the grooves for foreign objects.
The possibility depends on the profile, cord design, the diameter of the rollers and the specific belt routing. Counter-bending increases the bending load and must be included in the dimensioning. A roller on the belt back must have sufficient diameter and be positioned so that tooth engagement and grooveing are not impaired.
16 mm is the width of the supplier item whose SKU is used as the main product's stock reference. Other widths are handled as choices under the same product because they are cut from the same type of timing belt sleeve. The base width also determines the percentage-based pricing in the webshop.
The standard version is single-sided with teeth on the inside and a smooth back. It must run with the teeth in the corresponding tooth grooves; the back is not an alternative tooth side.
The steel cord tension members absorb the longitudinal tensile load and provide high longitudinal stiffness. This helps maintain pitch and position during operation. The cord must not be kinked, exposed or damaged during installation, as local damage can weaken the belt.
Check that the belt runs centrally, that there is no abnormal heat or noise, and that the edges are not constantly rubbing against the flanges. Also look for signs of too low or too high pretension. If the drive requires a re-tension check, the machine manufacturer's procedure must be followed.
This product is already GEN III. The reinforced version features high-performance PU and denser, two-filament steel cord construction and is a separate product line from the standard belt.
Conti Synchroflex AT10 GEN III 1050 is the correct size when the drive requires AT10 GEN III, 1050 mm pitch length and 105 teeth. The belt is cast endless in PU with steel cord and must be used with timing belt pulleys that match the profile. Choose the width according to the technical load and always check the design, alignment and pretension before commissioning.